
 English
 Español
 Français

If your finishing department is constantly fighting tight lead times, inconsistent surface quality, and rising labor costs, isotropic finishing can be a major upgrade—especially when paired with a centrifugal barrel finishing machine.
Unlike traditional vibratory finishing that’s optimized for large-batch throughput, a centrifugal barrel creates a much higher finishing energy inside a sealed barrel. That higher energy translates into a simple business outcome:
Shorter cycle time → higher throughput → lower labor cost → less rework → better ROI.
In this guide, you’ll learn what isotropic finishing is, why a centrifugal barrel is one of the fastest ways to achieve it, and how it reduces total finishing cost in real production.
What Is Isotropic Finishing?
An “isotropic” surface means the texture is uniform in all directions. In finishing terms, isotropic results are valued because they deliver:
More consistent appearance (even reflection, less directionality)
More stable functional performance (better contact behavior, smoother sliding, reduced micro-tearing)
Lower risk of “random” surface defects appearing after plating/coating or during use
Many manufacturers pursue isotropic results when the part is high-value or the surface requirement is strict—especially on precision metal components, complex geometries, and 3D printed parts.
 Example of an isotropic superfinish.
Why a Centrifugal Barrel Is Faster for Isotropic Finishing
1) Higher energy per minute (faster surface transformation)
A centrifugal barrel finishing system is designed to generate stronger processing forces than standard vibratory finishing. That higher energy means your parts and media interact more aggressively and efficiently inside each barrel—so the same result can often be achieved in a fraction of the time.
When cycle time drops, everything else improves:
capacity increases without adding labor
lead times become easier to control
finishing becomes less of a production bottleneck
2) Sealed, controlled environment (more predictable results)
Many centrifugal barrel systems operate in a sealed barrel environment, which helps keep the process controlled and repeatable:
stable media-to-part contact
reduced splashing and variability
more consistent batch-to-batch finishing behavior
3) Better fit for “high requirement / small-to-mid batch” jobs
Vibratory finishing is excellent for large-volume jobs, but when the goal is high-end surface quality with short delivery, the centrifugal barrel becomes the faster, more economical choice.
Common use cases:
high value machining parts
3D printed metal parts that need fast smoothing and polishing
parts that must look premium (appearance matters)
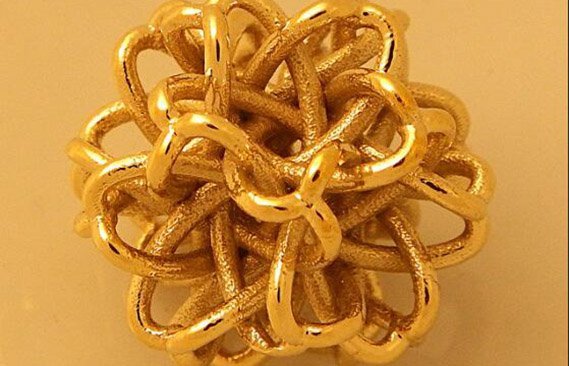 3D printed brass parts
Where the Cost Savings Really Come From (TCO Thinking)
Many buyers compare finishing machines by purchase price only. That’s a mistake.
The smarter comparison is Total Cost of Ownership (TCO). A faster isotropic finishing process improves TCO through four main levers:
1) Shorter cycle time = higher output per day
If one cycle becomes 30–70% shorter (depends on material, media, target finish), your finishing capacity increases immediately—often without changing headcount.
Result: you ship more with the same team and floor space.
2) Lower labor cost (less manual work per finished part)
Labor costs show up in:
loading / unloading
sorting / separation
cleaning / rework
repeated trial-and-error on parameters
Centrifugal barrel finishing helps reduce the “touch time” because cycles are shorter and results are more predictable. Many factories find they can consolidate finishing steps or reduce repeated rework.
3) Less rework and fewer rejects (quality becomes more stable)
When finishing is inconsistent, cost rises invisibly:
rework consumes time and labor
defects appear after coating/plating
surface mismatch triggers customer complaints
Isotropic finishing targets repeatable, uniform surface behavior, which reduces those late-stage quality surprises.
4) Faster response for urgent jobs (time becomes a competitive advantage)
If your customer needs faster lead time, the finishing department can become the limiting factor. A shorter isotropic finishing cycle gives you flexibility:
faster delivery
quicker sampling and approval
better response to rush orders
Time savings often become the real “profit savings.”
Conclusion: Isotropic Finishing Is a Productivity Upgrade, Not a “Nice-to-Have”
A centrifugal barrel finishing system can save time and cost because it:
produces higher finishing energy → shorter cycles
stabilizes results → less rework and fewer rejects
reduces labor pressure → easier scaling
improves delivery speed → stronger competitiveness
If your finishing step is slowing down production or eating labor budget, isotropic finishing is worth evaluating.
 gear parts before and after polishing
Want a fast recommendation?
Send us your part photos + material + size + target finish + daily output. We can suggest:
the right centrifugal barrel model
media & compound
starter parameters for your first production trial
Process Essentials: Why Media Choice Matters (High-Density Media Advantage)
A centrifugal barrel isn’t just a machine—it’s a system. The media and compound you choose determine whether you get fast results or expensive trial-and-error.
One key takeaway from isotropic workflows is that high-density media can help you reach the target surface faster because it transfers energy more efficiently.
High-density ceramic media is commonly chosen when you want:
stronger cutting/burnishing action per minute
shorter cycle time
stable, repeatable finishing behavior over many batches
Practical tip:
If you want isotropic results fast, don’t treat media as an afterthought. Use the right density and shape based on part geometry and the surface target.
Related reading:
- What Is Isotropic Finishing? Process, Benefits & Applications
- How to Choose the Right Mass Finishing System
- How to Estimate the Correct Mass Finishing Machine Capacity
- 3D Printed Parts Finishing: Methods, Media & Best Practices
- Tumbling Media Selection Guide: How to Choose the Right Media
- Surface Roughness Chart: Ra, Rz, RMS & N-Grade Conversion
