20+ Years of Excellence
Since 2003, Inovatec Machinery has been at the forefront of surface finishing technology innovation.
Inovatec Machinery · Vibratory Finishing
Inovatec’s Vibratory Deburring Machines give smooth surface finishes, fast deburring, and reliable results for every batch. Below is real performance data and before-and-after comparisons from our industrial customers.
Process Specs
| Part Material | Processing Time (minutes) | Media Type | Media Wear Rate | Before Ra | After Ra | Material Removal | Consistency | |
|---|---|---|---|---|---|---|---|---|
| Stainless Steel (304) | 60 minutes | GC Ceramic Media ACT 20X20mm (3/4 inch) | 0.5% per hour | 1.0 | 0.18 | < 0.3% | Surface uniformity ±1% |
Detailed specifications for our VBS(B) series vibratory deburring machines. Compare models and download comprehensive technical documentation.

| Model | VBS(B)100 | VBS(B)150 | VBS(B)200 | VBS(B)300 | VBS(B)400 | VBS(B)600 |
|---|---|---|---|---|---|---|
| Total Volume (L) | 100 | 150 | 200 | 270 | 400 | 600 |
| Maximum Overall Diameter (mm) A | 1080 | 1170 | 1200 | 1370 | 1470 | 1860 |
| Motor Mounting Tube (mm) B | φ460 | φ460 | φ530 | φ630 | φ630 | φ900 |
| Bowl Channel Width C (mm) | φ220 | φ260 | φ252 | φ275 | φ330 | φ390 |
| Discharge Width (mm) | 250 | 210 | 250 | 320 | 380 | 470 |
| Machine Height (mm) H1 | 980 | 860 | 940 | 960 | 1270 | 1140 |
| Discharge Height (mm) H2 | 800 | 710 | 770 | 760 | 1090 | 925 |
| Media Discharge Height (mm) H3 | 470 | 440 | 360 | 290 | 570 | 400 |
| Motor (kW) | 1.5/2.2 | 2.2 | 3.0 | 3.7/5.0 | 5.0/6.0 | 5.5/7.5 |
| Weight (kg) | 280 | 320 | 460 | 650 | 780 | 1180 |
Our efficient vibratory deburring machines feature a durable design and provide customizable vibratory finishing solutions to meet a wide range of industrial needs.
| Material / Part Type | Objective | Media | Compound | Time | Notes |
|---|---|---|---|---|---|
| Iron / 304 Stainless Steel | Deburring + Edge Smoothing | Ceramic Media ACT 20×20 (GC) | LC-13 | 1–2 Hours | Use a wet processing method; rinse after processing; adjust the time according to burr size and part fragility. |
| Aluminum Die Castings | Light Deburring + Surface Smoothing | 600 lb Plastic Media Cone | LC-13 | 30–60 Minutes | Softer parts—avoid over-cutting; if part-to-part scratching occurs, reduce the amplitude or speed. |
| Magnesium Alloy Die Castings | Light Deburring + Surface Smoothing | 600 lb Plastic Media Cone | LC-13 | 30–60 Minutes | A gentle mode is recommended; ensure thorough rinsing and drying to prevent staining. |
| Titanium Alloy Components | Deburring + Edge Finishing | Ceramic Media ACT 20×20 (FC) | LC-13 | 2 Hours | Titanium alloy is harder—ceramic media works better; extend the processing time for heavier burrs. |
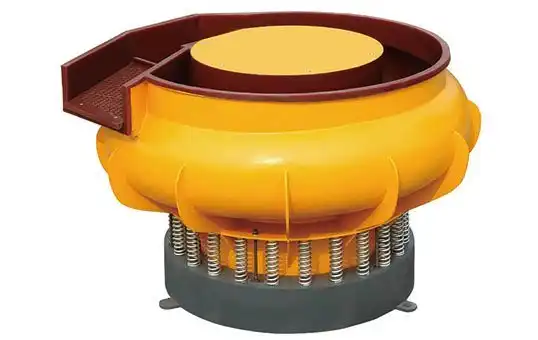
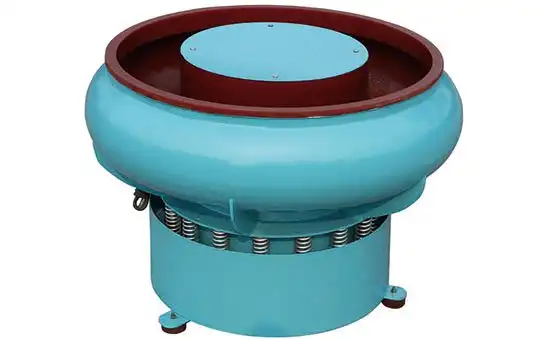
The VBS(B) uses a straight-wall bowl rather than a curved-wall design. This geometry allows a full-width separation deck to be fitted at the discharge opening, giving consistent screen coverage across the entire bowl exit. When the pneumatic shutter opens, all parts and media discharge onto the deck simultaneously — the screen retains parts and lets media fall through, achieving 100% separation without manual sorting. Screen hole sizes are customised to the specific part and media dimensions of your application.
The bowl interior is lined with 20 mm polyurethane throughout. At 20 mm thickness, the lining provides both wear resistance against abrasive ceramic media and structural cushioning that reduces transmitted vibration noise. The VBS(B) is available in six bowl sizes from 100 L to 600 L, with motor options ranging from 1.5 kW (VBS(B)100) to 7.5 kW (VBS(B)600). Selecting the right bowl size for your batch volume is the primary sizing decision — the rule of thumb is that parts and media together should fill 70–80% of the bowl volume at operating load.
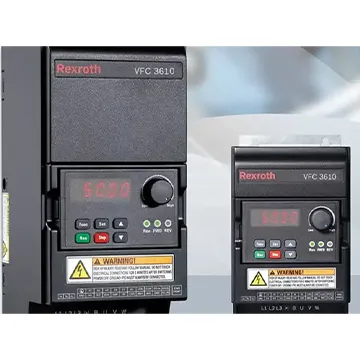
Variable frequency drive (VFD) speed control is available via a Bosch Rexroth inverter. Amplitude adjustment matters because different part materials require different intensity levels — aluminum and zinc die-cast parts process at lower amplitude to prevent part-on-part denting; steel and titanium parts can run at higher amplitude for faster burr removal. The VFD also enables soft start, which reduces mechanical stress on the springs and motor bearings at cycle start, extending service life in continuous production.
The VBS(B) is the straight-wall bowl model in the Inovatec vibratory finishing range — the defining difference from the VBS(A) spiral bowl is the discharge system. The straight-wall bowl allows a full-width separation deck and pneumatic shutter to be fitted, enabling automatic parts-and-media separation at the end of each cycle. This makes the VBS(B) the standard choice for production environments where manual sorting is not practical, and for applications where 100% media recovery is required to control running costs.
Our VBS(B) Vibratory Deburring Machine is designed for deburring and edge rounding aluminum, brass, copper, stainless steel, and iron workpieces, including machined parts, injection-molded parts, stamped parts, and die-cast parts.
In the vibratory deburring process, the working bowl loaded with workpieces, finishing media, and compound for wet processing is subjected to controlled rotary vibration. This motion creates continuous friction between the media and the workpieces, removing burrs, eliminating sharp edges, and improving surface smoothness with consistent results.
Vibratory deburring is one of the most cost-effective mass finishing methods because it can process large batches of parts with minimal operator involvement. Inovatec provides both batch and continuous vibratory deburring solutions. The discharge flap and separation screen quickly separate parts from media. The VBS(B) series is equipped with an extended separation deck and offers multiple screen hole options to accommodate different part sizes and media types.
Watch our Surface finishing process in action. Learn more about our Surface finishing process technology.
Our mass finishing machine and tumbling media serve diverse industries with specialized finishing solutions for various materials and part types.
Engine components, transmission parts, brake systems
Turbine blades, landing gear, structural components
Fasteners, connectors, precision tools
Post-processing, surface refinement, finishing
Inovatec Machinery stands out as a trusted partner in surface finishing solutions, offering unmatched quality, innovation, and customer support.
Since 2003, we've been at the forefront of surface finishing technology, continuously innovating and improving our solutions based on real-world manufacturing needs.
We understand that every application is unique. Our engineering team works closely with you to design and configure machines that perfectly match your requirements.
With partners and service centers worldwide, we provide localized support and rapid response times regardless of your location.
We value your time. Our technical team responds to inquiries within 24 hours, ensuring you get the answers and support you need quickly.
Benefit from our expertise at no cost. We offer complimentary technical consultations to help you optimize your finishing processes and select the right equipment.
Over 500 satisfied customers across 50+ countries trust Inovatec for their surface finishing needs, with a 99% customer satisfaction rate.
Explore real applications by industry and scenario, with Before/After, sub‑categories and resources to help you quickly find what you need.
Jewelry | Precious Metals | Jewelry Polishing
Precision polishing, deburring and mirror finishing for gold, silver, copper and titanium jewelry—balancing premium surface quality with throughput.
Burrs on edges, surface scratches and oxidation spots reduce luster and wearing comfort.
Noticeably improved mirror gloss with rounded edges and better wearing comfort.
Additive Manufacturing | SLA/SLS/FDM
Removes layer lines, densifies surfaces and unifies appearance for 3D‑printed parts across materials and processes.
Pronounced layer lines, support marks and rough surface affect assembly and appearance.
Smooth, refined surface ready for painting/electroplating; presentation‑grade look.
Sheet Metal | Laser Cutting | Edge Optimization
Removes dross/burrs and adds edge radiusing on laser‑cut parts to improve safety and assembly quality.
Sharp, burred edges can cause cuts and hinder coating adhesion.
Consistent rounded edges and clean surfaces for better paint/e‑coat adhesion.
Consumer Electronics | Small Appliances | Exterior Parts
Delivers consistent texture and feel for high‑volume consumer products, improving brand perception and yields.
Uneven brushing, micro‑burrs and harsh feel affect assembly and user experience.
Uniform texture, smooth edges and refined touch; markedly better consistency.
Stone | Gemstone | Tumbling
Rounds edges and enhances gloss on natural/synthetic stones for jewelry and decorative crafts.
Sharp edges, rough surfaces and uneven color/reflection.
Rounded edges and even polish; improved visual appeal.
Automotive | Engine/Drivetrain | High‑volume Consistency
Deburring, edge radiusing and surface consistency for automotive parts to meet stringent standards.
Tool marks and residual burrs with sharp edges reduce fatigue strength and hinder assembly.
Stable edge radii and compliant roughness with high repeatability.
Defense | High Reliability | Process Consistency
High‑reliability, consistent surface finishing across metals and composites.
Sharp edges, stress concentrations and surface defects impact durability and safety.
Consistent chamfers and stable surface quality; coating/assembly‑ready.
Aluminum Profiles | Die‑cast Parts | High‑volume Finishing
Efficient, consistent finishing for aluminum parts; ideal for pre‑anodizing treatment and brushed/polished appearance.
Gate/flash marks and dull surfaces; notable batch variation.
Flash removed with refined texture and higher brightness; improved batch consistency.
Engineering Plastics | Injection‑molded Parts | Deflashing
Removes plastic flash and smooths edges to prevent scratching and improve assembly.
Visible flash and sharp edges affect feel and assembly.
Flash removed and corners smoothed; improved look and feel.
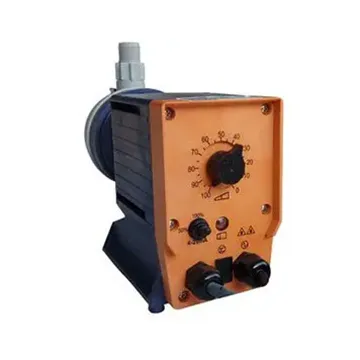
Enhance your mass finishing machine and tumbling media with our professional-grade accessories. Increase efficiency, reduce noise, and optimize your finishing process.
Get the most out of your mass finishing machine and tumbling media with our comprehensive accessory package. Our experts will help you select the right combination of accessories for your specific application needs.
Accessories designed to maximize machine efficiency and output quality
Reduce operational costs through improved efficiency and reduced waste
All accessories designed for seamless integration with your existing machine
Inovatec Machinery is committed to the highest standards of quality, safety, and reliability.
Quality Management System certified by international standards, ensuring consistent product quality.
European Conformity marking ensuring our machines meet EU safety standards.
Comprehensive testing and inspection reports from SGS.
Environmental protection standards compliance.
Since 2003, Inovatec Machinery has been at the forefront of surface finishing technology innovation.
Our machines are trusted by manufacturers worldwide and recognized at major industry exhibitions.
Regular participation in major industry exhibitions worldwide.
Strategic partnerships across major manufacturing regions.
Find answers to common questions about our products.
A vibratory deburring machine uses vibration and abrasive media to remove sharp edges, burrs, and surface imperfections from metal, plastic, or ceramic parts. It is ideal for batch processing of small to medium-sized components.
The machine generates controlled vibrations that cause the parts and deburring media to rub against each other in a circular or elliptical motion, resulting in uniform edge breaking and surface smoothing.
Commonly processed parts include metal stampings, machined components, die-cast parts, 3D printed parts, and plastic or aluminum components requiring edge deburring, rust removal, or polishing.
Typical media includes ceramic, plastic, stainless steel, or natural materials. The selection depends on the part material, desired finish, and processing goals (deburring, polishing, cleaning, etc.).
Yes. By adjusting vibration amplitude, cycle time, and choosing the correct media, vibratory deburring can be tuned for precision parts without damaging tolerances or surface integrity.
Most vibratory deburring machines support wet processing with water and compound for better cleanliness and surface finish. Dry processing is possible with media like walnut shells but requires specific setups.
Cycle time varies from 15 minutes to 2 hours, depending on the part size, material, burr severity, and required finish. Trial runs are recommended for optimal results.
Regular maintenance includes checking PU lining wear, inspecting vibration motors, greasing bearings, cleaning the drain system, and replacing worn media. Proper upkeep ensures consistent performance.
Yes. Vibratory deburring machines can be integrated with loading/unloading systems, compound dosing pumps, PLC controls, and conveyor lines for high-volume automated finishing.
The primary sizing factor is your daily batch volume in kilograms or parts per hour, combined with the largest part dimension. As a starting point: VBS(B)100 (100 L) suits small workshops processing up to 50 kg/batch; VBS(B)200 (200 L) is a common production choice for 100–150 kg/batch; VBS(B)400–600 L models suit high-volume production lines processing 200 kg/batch or more. The key constraint is that parts and media combined should fill 70–80% of bowl volume — underfilling produces inconsistent results, overfilling reduces vibration amplitude. Send us your part dimensions, material, daily target volume and required finish, and we size the bowl and motor within 24 hours.
| Parameter | Specification |
|---|---|
| Speed range (RPM) / amplitude (mm) | Motor RPM 0–1480 (VFD optional) / Vibration amplitude 0–10 mm |
| Timer range | 0–24 hours |
| Electrical options (Voltage/Hz) | 208V–480V, 50/60Hz |
| Noise level (with/without soundproof cover) | 75–90 dB (depends on load, media, cover, and installation) |
| PU lining thickness | 20 mm PU lining |
| Wear parts (typical) | Springs, motor bearings |
| Water inlet / compound inlet | Optional — specify inlet size (e.g., 1/2” or 3/4”) |
| Drain outlet | Optional — specify drain size (e.g., 1” or 1-1/2”) |
| Discharge method | Manual flap (standard) / Pneumatic shutter (optional) |
| Separation method | Separator deck with custom screen hole sizes (optional) |
| Screen hole options | Custom screen hole size based on part & media size |
| Recommended media-to-parts ratio | Typical: 3:1 to 5:1 (media:parts by volume) (test required) |
The VBS(A) is a spiral-bowl design optimised for ball burnishing and polishing — its 3D toroidal media flow produces a high-luster surface finish and allows 100% parts-and-media separation via an external separator. The VBS(B) is a straight-wall bowl designed primarily for deburring and edge rounding — its geometry supports an integrated separation deck and pneumatic shutter for in-machine automatic discharge, which simplifies the line layout and reduces floor space. Choose VBS(A) when your priority is surface brightness and burnishing quality. Choose VBS(B) when your priority is deburring throughput with automated in-machine separation, particularly for stamped, machined or die-cast metal parts processed in large batches.
Ready to improve your finishing process? Contact our experts for a personalized quote and technical consultation.
Fill out the form below and our team will contact you within 24 hours.
Prefer to contact us directly? Choose your preferred method.
Ready to experience the Inovatec difference? Contact our team for personalized solutions.
399# Shushan Road, Wuxing District, Huzhou City, Zhejiang Province, 313000 China
6317 Arcadia St, Eastvale, CA 92880 USA (323-577-3309)
Read reviews and see our business information on Google.
View Google Business