20+ Years of Excellence
Since 2003, Inovatec Machinery has been at the forefront of surface finishing technology innovation.
Inovatec Machinery · Vibratory Finishing
Inovatec’s Rotary Barrel Tumbling Machines give smooth surface finishes, fast deburring, and reliable results for every batch. Below is real performance data and before-and-after comparisons from our industrial customers.
Process Specs
Parts Material | Processing time (min) | Media Type | Media Wear Rate | Ra before | Ra after | Material Removal | Consistency | |
Stainless steel (304) | 120 minutes | Fine porcelain Pins 2X8mm | 0.2% per hour | 1.0 | 0.2 | < 0.2% | ±1% Surface Uniformity |
Consistent Results: The rotary barrel tumbling machine delivers uniform surface finish quality from batch to batch, ensuring stable and reliable results in mass production.
Low Damage Rate: With gentle tumbling action and properly selected media, the rotary barrel tumbling machine reduces part-to-part impact, making it suitable for small or delicate components.
High Repeatability: Digital controls and simple program settings help the rotary barrel tumbling machine maintain cycle-to-cycle consistency, typically within ±1% under identical processing conditions.
Real Industrial Testing: The rotary barrel tumbling machine is proven by 1,000+ finishing tests across different metals, part sizes, and geometries.
Process Tracking: Each rotary barrel tumbling machine can record cycle time, media type, and key process parameters for easier quality control and repeatable production.
Detailed specifications for our DM series barrel tumbling machines. Compare models and download comprehensive technical documentation.
| Model | Capacity | Size | Motor | Weight | Speed | Lining thickness |
| (L) | LxWxH(mm) | (kw) | (kg) | (rpm) | (mm) | |
| DM25 | 25 | 680x700x750 | 0.55 | 100 | 85 | 8 |
| DM50 | 50 | 730x720x1200 | 1.1 | 150 | 60 | 8 |
| DM100 | 100 | 1020x900x1300 | 1.1 | 200 | 40 | 10 |
| DM200 | 200 | 1090x1000x1420 | 2.2 | 500 | 30 | 10 |
| DM300 | 300 | 1450x1000x1420 | 2.2 | 560 | 30 | 10 |
| DM500 | 500 | 1660x1300x1520 | 2.5 | 1000 | 20 | 10 |
The DM series rotary barrel tumbling machine uses slow rotation rather than vibration to generate finishing action — parts and media tumble together as the hexagonal barrel rotates. This gentler process is the key reason to choose barrel tumbling over vibratory finishing for specific applications. The three design elements below determine practical output.
The DM series uses a hexagonal barrel cross-section. The flat faces of the hexagon create a consistent lift-and-drop tumbling action as the barrel rotates — parts and media are lifted up the face, then cascade down as the barrel turns. This cascade motion generates more uniform media-to-part contact than a circular barrel, which tends to allow parts to slide rather than tumble. The barrel speed is low — 20 to 85 rpm depending on model — producing a gentle action that significantly reduces part-to-part collision energy compared with vibratory finishing.
The barrel interior is lined with 8–10 mm cast PU throughout. The PU lining protects parts from metal-on-metal contact with the barrel wall and absorbs impact noise. The DM series covers six barrel sizes from DM25 (25 L, 0.55 kW, 85 rpm) to DM500 (500 L, 2.5 kW, 20 rpm). Note that barrel speed decreases as barrel size increases — this is by design: larger barrel diameter means higher tangential velocity at the same rpm, so lower rpm maintains an equivalent surface speed and prevents parts from centrifuging against the wall instead of tumbling.
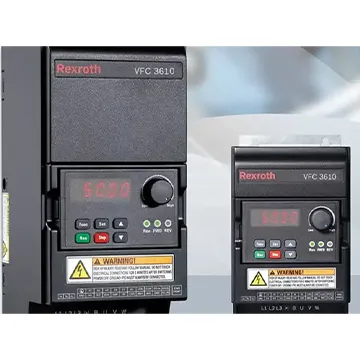
All DM models include a hinged safety cover that prevents access to the rotating barrel during operation. The digital process timer allows the operator to set cycle time and walk away; the machine stops automatically at end of cycle. An optional Bosch Rexroth variable frequency drive (VFD) allows rotation speed adjustment without changing hardware — useful for tuning process intensity when switching between heavy deburring (higher speed) and dry polishing (lower speed).
The DM series rotary barrel tumbling machine is the oldest and simplest mass finishing technology — and it remains in widespread use because it is the gentlest of all finishing machine types. Where vibratory machines drive media against parts through high-frequency vibration, the rotary barrel simply rotates the entire barrel at low speed, allowing parts and media to tumble together by gravity. Part-to-part collision energy is low, making barrel tumbling the standard choice for thin stampings, delicate parts with fragile geometry, parts with holes, and long or sensitive components where vibratory action risks denting or scratching.
The trade-off is cycle time: barrel tumbling typically runs 1–10 hours per cycle, compared with 15 minutes to 2 hours for vibratory finishing. For applications where part quality takes priority over throughput — burnishing of brass fixtures, dry polishing of jewelry, finishing of acrylic or wood parts — this trade-off is acceptable.
Rotary barrel tumbling machines are the oldest way of surface finishing. Yet, it is still widely used because of its low cost. Barrel sizes range from small size as 25L to huge barrel size 500L.
In barrel tumbling process, the rotary drum rolls the mass in the barrel and parts get the desired surface. The process usually takes hours or even days. After all, barrel process is available either wet or dry or even without media.
Barrel tumbling machines are available in Hexagonal shape and Olive shape.
Feature:
Applications:
Watch our Surface finishing process in action. Learn more about our Surface finishing process technology.
Our mass finishing machine and tumbling media serve diverse industries with specialized finishing solutions for various materials and part types.
Engine components, transmission parts, brake systems
Turbine blades, landing gear, structural components
Fasteners, connectors, precision tools
Post-processing, surface refinement, finishing
Inovatec Machinery stands out as a trusted partner in surface finishing solutions, offering unmatched quality, innovation, and customer support.
Since 2003, we've been at the forefront of surface finishing technology, continuously innovating and improving our solutions based on real-world manufacturing needs.
We understand that every application is unique. Our engineering team works closely with you to design and configure machines that perfectly match your requirements.
With partners and service centers worldwide, we provide localized support and rapid response times regardless of your location.
We value your time. Our technical team responds to inquiries within 24 hours, ensuring you get the answers and support you need quickly.
Benefit from our expertise at no cost. We offer complimentary technical consultations to help you optimize your finishing processes and select the right equipment.
Over 500 satisfied customers across 50+ countries trust Inovatec for their surface finishing needs, with a 99% customer satisfaction rate.
Explore real applications by industry and scenario, with Before/After, sub‑categories and resources to help you quickly find what you need.
Jewelry | Precious Metals | Jewelry Polishing
Precision polishing, deburring and mirror finishing for gold, silver, copper and titanium jewelry—balancing premium surface quality with throughput.
Burrs on edges, surface scratches and oxidation spots reduce luster and wearing comfort.
Noticeably improved mirror gloss with rounded edges and better wearing comfort.
Additive Manufacturing | SLA/SLS/FDM
Removes layer lines, densifies surfaces and unifies appearance for 3D‑printed parts across materials and processes.
Pronounced layer lines, support marks and rough surface affect assembly and appearance.
Smooth, refined surface ready for painting/electroplating; presentation‑grade look.
Sheet Metal | Laser Cutting | Edge Optimization
Removes dross/burrs and adds edge radiusing on laser‑cut parts to improve safety and assembly quality.
Sharp, burred edges can cause cuts and hinder coating adhesion.
Consistent rounded edges and clean surfaces for better paint/e‑coat adhesion.
Consumer Electronics | Small Appliances | Exterior Parts
Delivers consistent texture and feel for high‑volume consumer products, improving brand perception and yields.
Uneven brushing, micro‑burrs and harsh feel affect assembly and user experience.
Uniform texture, smooth edges and refined touch; markedly better consistency.
Stone | Gemstone | Tumbling
Rounds edges and enhances gloss on natural/synthetic stones for jewelry and decorative crafts.
Sharp edges, rough surfaces and uneven color/reflection.
Rounded edges and even polish; improved visual appeal.
Automotive | Engine/Drivetrain | High‑volume Consistency
Deburring, edge radiusing and surface consistency for automotive parts to meet stringent standards.
Tool marks and residual burrs with sharp edges reduce fatigue strength and hinder assembly.
Stable edge radii and compliant roughness with high repeatability.
Defense | High Reliability | Process Consistency
High‑reliability, consistent surface finishing across metals and composites.
Sharp edges, stress concentrations and surface defects impact durability and safety.
Consistent chamfers and stable surface quality; coating/assembly‑ready.
Aluminum Profiles | Die‑cast Parts | High‑volume Finishing
Efficient, consistent finishing for aluminum parts; ideal for pre‑anodizing treatment and brushed/polished appearance.
Gate/flash marks and dull surfaces; notable batch variation.
Flash removed with refined texture and higher brightness; improved batch consistency.
Engineering Plastics | Injection‑molded Parts | Deflashing
Removes plastic flash and smooths edges to prevent scratching and improve assembly.
Visible flash and sharp edges affect feel and assembly.
Flash removed and corners smoothed; improved look and feel.
Enhance your mass finishing machine and tumbling media with our professional-grade accessories. Increase efficiency, reduce noise, and optimize your finishing process.

Get the most out of your mass finishing machine and tumbling media with our comprehensive accessory package. Our experts will help you select the right combination of accessories for your specific application needs.
Accessories designed to maximize machine efficiency and output quality
Reduce operational costs through improved efficiency and reduced waste
All accessories designed for seamless integration with your existing machine
Inovatec Machinery is committed to the highest standards of quality, safety, and reliability.
Quality Management System certified by international standards, ensuring consistent product quality.
European Conformity marking ensuring our machines meet EU safety standards.
Comprehensive testing and inspection reports from SGS.
Environmental protection standards compliance.
Since 2003, Inovatec Machinery has been at the forefront of surface finishing technology innovation.
Our machines are trusted by manufacturers worldwide and recognized at major industry exhibitions.
Regular participation in major industry exhibitions worldwide.
Strategic partnerships across major manufacturing regions.
Find answers to common questions about our products.
A rotary barrel tumbling machine is a mass finishing system used for deburring, descaling, polishing, or cleaning metal and plastic parts. It consists of a horizontal hexagonal or octagonal barrel that rotates at a controlled speed. As the barrel turns, parts tumble against abrasive media, resulting in surface refinement through friction and impact.
| Material / Part | Goal | Media | Compound | Wet/Dry | Time |
|---|---|---|---|---|---|
| Stainless steel stampings | Deburr + edge radius | Ceramic angle-cut | LC series (or “compound optional”) | Wet | 2–6 hrs |
| Aluminum die cast | Smooth + light polish | Plastic cones (fine) | Mild compound | Wet | 1–4 hrs |
| Brass / copper parts | Bright polish | Porcelain ball | Burnishing compound | Wet | 1–3 hrs |
| Small parts with holes | Uniform finish | Small ceramic/plastic | As needed | Wet | 2–8 hrs |
| Dry polishing | Brighten + dry | Walnut shell / corncob | Polishing paste | Dry | 2–10 hrs |
| Item | Barrel Tumbling (Rotary / Drum) | Vibratory Finishing (Vibratory Bowl/Tub) |
|---|---|---|
| Motion | Parts + media tumble/roll in a rotating drum | Parts + media rub/flow under vibration |
| Best for | Gentle finishing, delicate parts, burnishing, long cycles | Fast deburring, edge radiusing, high throughput |
| Cycle time | Usually longer (1–10+ hrs) | Usually shorter (15 min–4 hrs) |
| Part damage risk | Lower (less aggressive, less part-on-part) | Can be higher for thin/delicate parts (needs good media choice & fixturing) |
| Part size range | Small to medium parts; very large parts less common | Very flexible; bowl/tub can handle larger parts well |
| Separation | Often manual or batch separation | Easier automation: screens, separation decks, continuous flow options |
| Noise | Generally quieter than vibratory | Usually louder (sound cover helps) |
| Typical media | Ceramic, plastic, steel, walnut/corncob | Ceramic, plastic, porcelain, steel, organic media |
| Best use cases | Jewelry, precision parts, parts with fragile edges | Stamping, machining, die casting, high-volume deburring |
Pick a barrel tumbler when you want a gentler process:
Thin stampings, delicate parts, parts that scratch easily
Burnishing with steel media (bright finish + surface densification)
Dry polishing with walnut shell/corncob + paste
You can accept longer cycle times for a safer finish
Pick a vibratory finisher when you need speed and production efficiency:
Fast deburring / edge radiusing on machined, stamped, or die cast parts
Higher throughput and easier separation/automation
Multi-step processing (deburr → smooth → polish) with media changes
You want consistent results with shorter cycles
Need speed / heavy burr removal? → Vibratory finishing
Need gentler action / better part protection? → Barrel tumbling
Barrel tumbler for metal finishing is a cost-effective solution for deburring, edge radiusing, cleaning, burnishing, and polishing small-to-medium metal parts in batch production. In a rotary barrel tumbler, workpieces and media tumble together inside a rotating drum, delivering uniform surface results with minimal labor. Compared with vibratory finishing, barrel tumbling is gentler and helps reduce part-on-part damage—especially for delicate stampings, small machined parts, and components with holes.
Our rotary barrel tumbling machines support wet finishing (with water + compound) for deburring and cleaning, and dry finishing (walnut shell/corncob + polishing paste) for brightening and final shine. Multiple barrel shapes and capacities are available, with options such as PU lining, timer, variable speed, and custom voltage for your factory.
| Item | Wet Barrel Tumbling | Dry Barrel Tumbling |
|---|---|---|
| Best for | Deburring, cleaning, rust removal, edge radiusing, pre-polish | Final brightening, gentle polishing, drying-sensitive parts, shine enhancement |
| Media | Ceramic / plastic / steel (burnishing) | Walnut shell / corncob / wood media + polishing paste |
| Liquid | Water + compound (optional) | No water (paste or powder only) |
| Surface action | Stronger cutting + washing action | Softer, gentler “buffing” action |
| Typical cycle time | 0.5–6 hours (depends on burr size) | 1–10 hours (depends on gloss target) |
| Finish result | Matte → satin → pre-polish (depending on media) | Satin → bright → high gloss (best as final step) |
| When not ideal | Parts that trap water or cannot be dried | Heavy burrs, oily/dirty parts, strong deburring needs |
Choose wet tumbling when you need material removal + cleaning:
Remove burrs on stampings and machined parts
Smooth sharp edges / edge radiusing
Remove oxidation, cutting oil, dust
Burnishing with steel media (bright finish + densification)
Typical wet setup: ceramic or plastic media + water + compound, then rinse and dry.
Choose dry tumbling when you want a final cosmetic finish:
Brighten surfaces after wet deburring
Dry polish delicate parts (lower risk of water marks)
Avoid corrosion risk on parts that are hard to dry
Improve shine using walnut shell/corncob + polishing paste
Typical dry setup: walnut shell or corncob + polishing paste for 2–8 hours.
Wet deburr → rinse → dry → dry polish/brighten
This gives fast deburring and the best appearance.
Model selection is primarily driven by your batch weight and part size.
DM25 (25 L, 85 rpm): small batch trials, sample testing, jewelry and small hardware in quantities up to 5–8 kg per batch. Fastest rotation — best for harder, smaller parts.
DM50 (50 L, 60 rpm): small workshop standard. Up to 15–20 kg parts per batch. Suitable for brass, aluminum and small steel parts.
DM100 (100 L, 40 rpm): mid-size workshop. Up to 30–40 kg per batch. Good general-purpose size for hardware, castings and mixed batches.
DM200 (200 L, 30 rpm): higher volume; 60–80 kg per batch. Suitable for production-scale dry polishing and wet deburring.
DM300 (300 L, 30 rpm): large batch wet or dry finishing; up to 100 kg per batch.
DM500 (500 L, 20 rpm): highest volume model; up to 150–200 kg per batch. Low rotation speed — best for large, heavy parts or very large dry polishing batches.
General rule: fill the barrel 40–50% with media, then add parts to bring total load to 60–70% of barrel volume. Overfilling prevents tumbling; underfilling allows excessive part-to-part impact.
Ready to improve your finishing process? Contact our experts for a personalized quote and technical consultation.
Fill out the form below and our team will contact you within 24 hours.
Prefer to contact us directly? Choose your preferred method.
Ready to experience the Inovatec difference? Contact our team for personalized solutions.
399# Shushan Road, Wuxing District, Huzhou City, Zhejiang Province, 313000 China
6317 Arcadia St, Eastvale, CA 92880 USA (323-577-3309)
Read reviews and see our business information on Google.
View Google Business