
 English
 Español
 Français
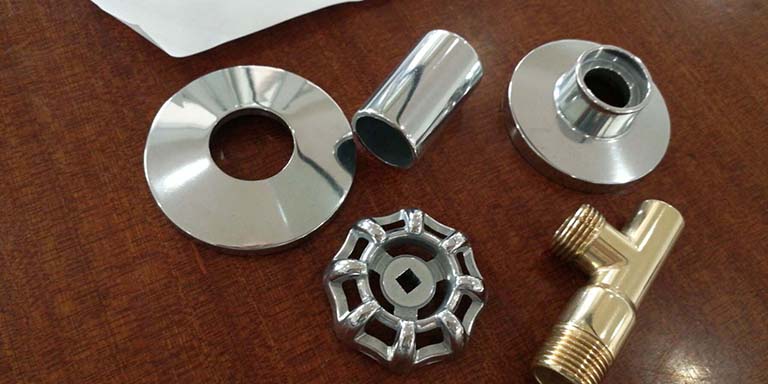
A few days ago, I received a request from Ayman about Zamak3 faucet parts zinc polish.
Ayman told me that the parts’ surface should be as smooth as possible because he will do electroplating after the mass finishing process.
He plans to send us a parcel of the samples to do the trial in our test room.
If the sample performance is suitable for plating, he will visit our factory in 2 weeks.
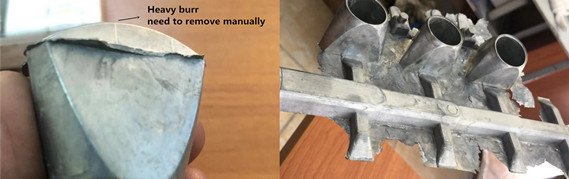
Zamak3 faucet parts received from the die casting machine
Ayman has several hot die casting machines in the workshop.
Some of the machines are old design manual die-casting while some others are CNC controlled.
We agree to take the photo of the sample and keep record after each process.
And in 3 days I received the sample from Ayman.
1. We check the surface condition of Zamak3 sample
When we check the parts, we found the surface is rough with some significant flash need to get rid of.
The parts size is the medium range, and the production capacity is big (about 3000 pcs per day in 8 hours).
Based on the information above, we start with the vibratory finishing process.
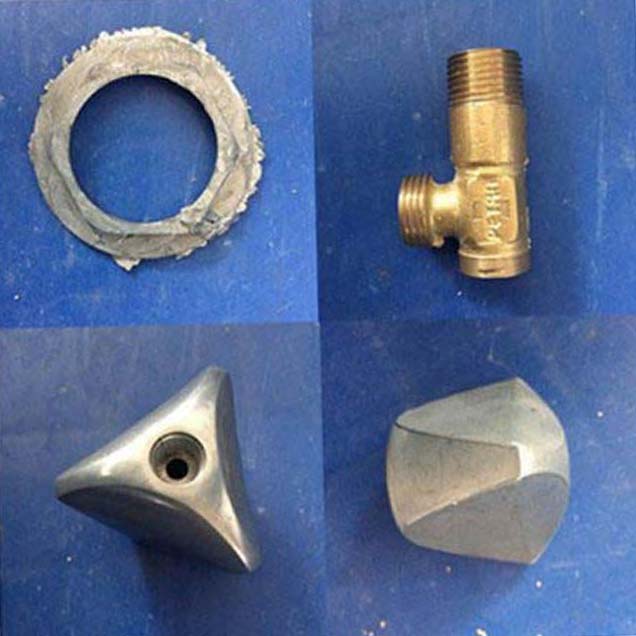
Zinc parts before surface finishing
Besides, we notice that some parts have an excellent initial condition while others have lousy surface quality.
I talk to Ayman about this finding, the reason is: some of the molds have been using for a long time.
2. We remove the burrs in the first stage
General burr removal is carried out with ceramic media.
Usually, this is the first step of metal finishing, such as steel, iron, and titanium.
The process takes about 2 hours.
After that, we can see significant burrs are cleared.

Zinc deburring with ceramic media
However, those vast flashes are challenging to remove with the vibratory finishing process.
Instead, they should be removed with a wheel grinding machine before putting into a vibratory finishing machine.
3. Parts smoothing with plastic tumbling media at the second stage
After burr removal is a smoothing process.
The smoothing process carried out in plastic media for 2 hours to reduce surface roughness and Ra value.
Therefore the surface is preferable for electroplating and nickel plating.
Below you can see the surface after the plastic smoothing process:

Zinc polish with plastic media
4. Sanitary Parts Polishing at the third stage
The zinc polish process takes only 20-30 minutes. Some manufacturers don’t use this process.
Because they only do electroplating and anodizing afterwards.
This coating is long-lasting and brighter than the polished surface.

Zinc polish with zirconia ball
A higher media to parts ratio is suggested to prevent parts impingement.
Typically we use 8:1 media to parts by volume.
A round vibratory finisher without separation gate is preferred to avoid parts damage during the separation sieve.
The finished parts are collected manually with operators.
5. Tip for Ayman: big casting flashes need to remove with grinding wheel
The deburring process takes about 2 hours.
However, only the loose burr and thin burr are removed.
Those thick flashes are not possible to clean even after very long tumbling time.
Because the vibratory finishing process removes metal material on the entire surface of the parts to the same level.
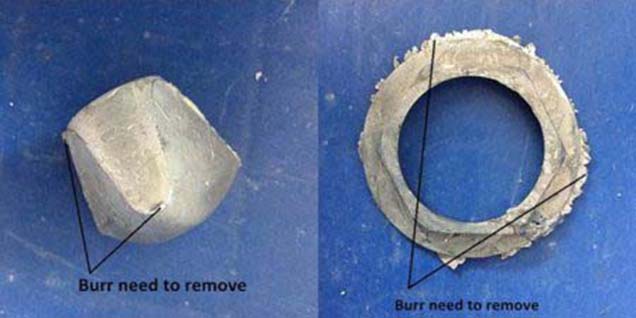
Burr removal of zinc parts
Although wheel grinding is a manual process, it saves time for the following vibratory tumbling process and improves output product quality.
6. Important: prevent lodging
The media lodging is really a painful issue for workshop owner.
It takes time and labor work to recover the parts. Therefore, the right selection of media size and shape is essential.
In this case, we would see that:
- The handles and taps don’t have a unique surface (only 15 mm hole).
- Valves we have 4 mm hole for water running through, 30 mm opening at the bottom. 10 mm hole at the top.
- For washer parts, we can basically use any angle cut ceramic media with a smaller size.
In the first place, cone shape ceramic media and plastic media is preferred because of no lodging.
However, cone shape media with a special shaping process, so it has a higher cost than other media shapes.
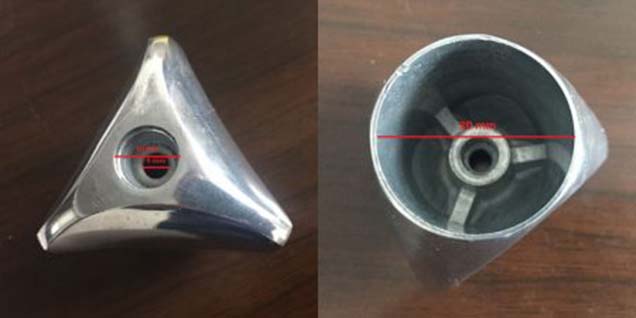
The surface configuration of zinc-parts
If you are concerned about the cost, then T/P shape media (a mixture of TET tetrahedron and pyramid) is a better choice.
Besides, cylinder wedge shape media also suggested because of less possibility of lodging than T/P shape media. 25 mm or 20 mm ceramic media for long service life.
Cone shape plastic media is the most common shape and cheap to make.
So we can use 20 mm or 25 mm cone shape.
7. Cost saving with media recycling
Parts lodging causes lots of labor work to recover the parts.
If an opening size 30 mm, when media size reduces down to 15 mm, it susceptible to lodging.
Therefore, we should remove the undersized media to avoid this with a vibratory separator.
However, those media are just in a smaller size, they are in good condition.
Simply throw them away is not a good idea.
If you check all the parts at hand, you will find that washer parts without any hole or cavity.
So this small size media can use for parts with simple surface geometry.
8. Selecting the right mass finishing equipment
Choosing the correct equipment is vital for a successful project.
The experience we learn from this case as follow:
- Surface finishing in a short time
- Finish all required job (3000 pcs per day)
- Save the labor work
In this case, we suggest a 600L round vibratory finishing machine instead of vibratory finishing machine with separation deck.
Because in the machine with separation deck (internal separation) parts and parts will hit and scratch.
Zamak3 alloy as a soft material makes the situation even worse.
This will finally affect nickel plating performance after the smoothing step.
To make it easier for parts collection, we suggest Ayman install a speed converter (Variable Frequency Drive).
So the workers can pick the parts easily when the vibration slows down.
The vibratory dryer is another equipment that we recommend.
Because zinc material is easy to rust when exposing to air environmental.
As a result, it needs immediate drying after the wet process.
We have more automatic surface finishing solutions that you can check.
All those solutions are according to practical requirement.
