
 English
 Español
 Français
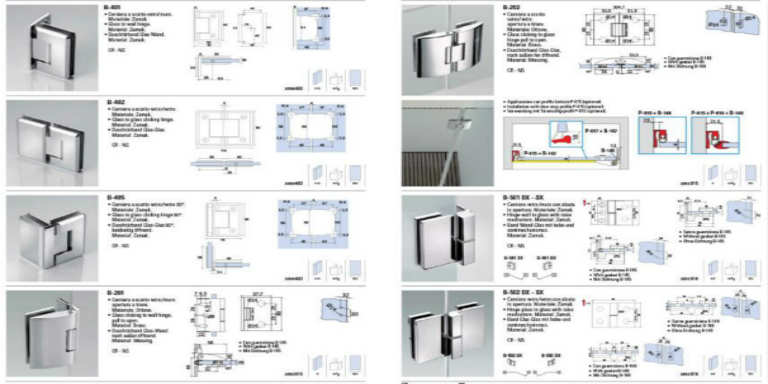
Zamak3 is the de facto standard for zinc alloys for the Zamak series, compared to all other zinc alloys.
Zamak 3 has the base composition for the Zamak alloys (96% zinc, 4% aluminum). It has excellent castability and long-term dimensional stability.
Because of its strength, ductility, and excellent plating and finishing character, Zamak 3 is a widespread indoor handle, door hinges, belt buckles, sliders, etc.
This article shows the process of how to finish the Zamak 3 furniture hinges from casting.
1. Parts condition before finishing
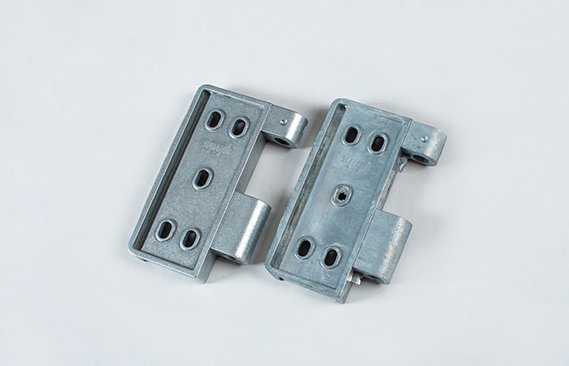 | Material: zamak3 die casting parts Appearance: dull and grey. De-molding burr at the edge and around the hole Shape: heavy parts with simple geometry. This part has multiple holes, so we need to take care to prevent undersized media login in. Size: customized Process before: die casting Process after: electroplating |
2. Parts surface requirement
- Smooth surface and low Ra value
- Remove loose burr generated from die casting
- Avoid parts hitting
- Avoid media lodge in
3. How we process the parts
| Step | (1) Deburring | (2) Drying |
| Machine | Vibratory finishing machine without separation | Vibratory dryer |
| Tumbling Speed | 50/60HZ (full speed) | 50/60HZ (full speed) |
| Chip Type | Plastic media 20×20 Cone Middle cutting | Corn Cob tumbling media |
| Media to Parts Ratio | 6:1 | 6:1 |
| Compound Type | LC-13 pH 8.5 (mild grinding compound) | |
| Water Level | Just cover the mass | |
| Tumble Time | 1.5 hours | 10 mins |
| Notes— | Manually take the parts out of the vibratory bowl | With PVC (or Nylon) separation sieve |
4. Parts condition before and after polishing
After the vibratory deburring process, the loose scales at the edge are removed. The entire surface is now matte finish texture.
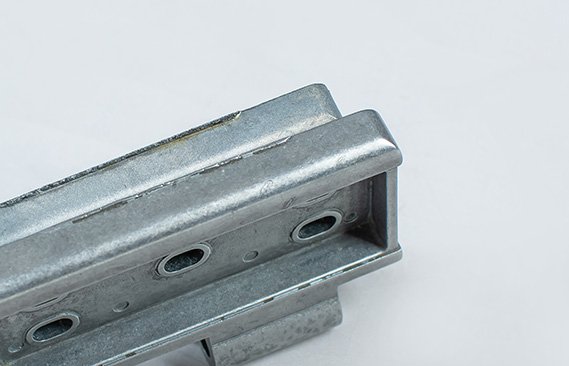
You could also see from the side; the part has a de-molding line (parting line) that can not be removed with the mass finishing process. This heavy burr has to release by the wheel grinding process manually before vibratory mass finishing.
5. Other considerations
This Zamak 3 part is quite heavy, so the media and parts ratio should higher to prevent parts from hitting each other.
The Zamak 3 parts are very easy to corrosion. So parts need to dry as soon as the deburring process finishes.
Some manufacturers introduce the dry tumbling process to deburr with a rubber-based plastic media. When you use this dry tumbling process, no water is involved. Again, their vibratory finishing machine is equipped with an extra dust collection device.
6. Conclusion
This article introduces an example of Zamak’s three parts of deburring and smoothing. Firstly, we show the condition of the parts before tumbling.
Then we talk about parts surface requirement, the process to improve the finish, comparison before and after finishing in turn.
Finally, we also discuss the dry tumbling process as an excellent way to finish the Zamak 3 parts.
